Intero Integrity Services, Belgium: Pipeline Refill and Nitrogen Separation
Challenge
Intero Integrity Services required surface separation support for the refilling of a pipeline in Belgium. The pipeline was filled with nitrogen and kerosene. The plan was to refill the line with kerosene by means of a pig, propelled with kerosene from one specific location towards the receiving station.
At the receiving end, the incoming kerosene had to be separated from the nitrogen ahead of the pig. The kerosene was to be recovered into a storage tank for return to the line, while the nitrogen had to be vented in a safe and controlled manner. The operation required precise pressure control to keep the pig moving at a stable speed, and execution was required on very short notice.
Solution
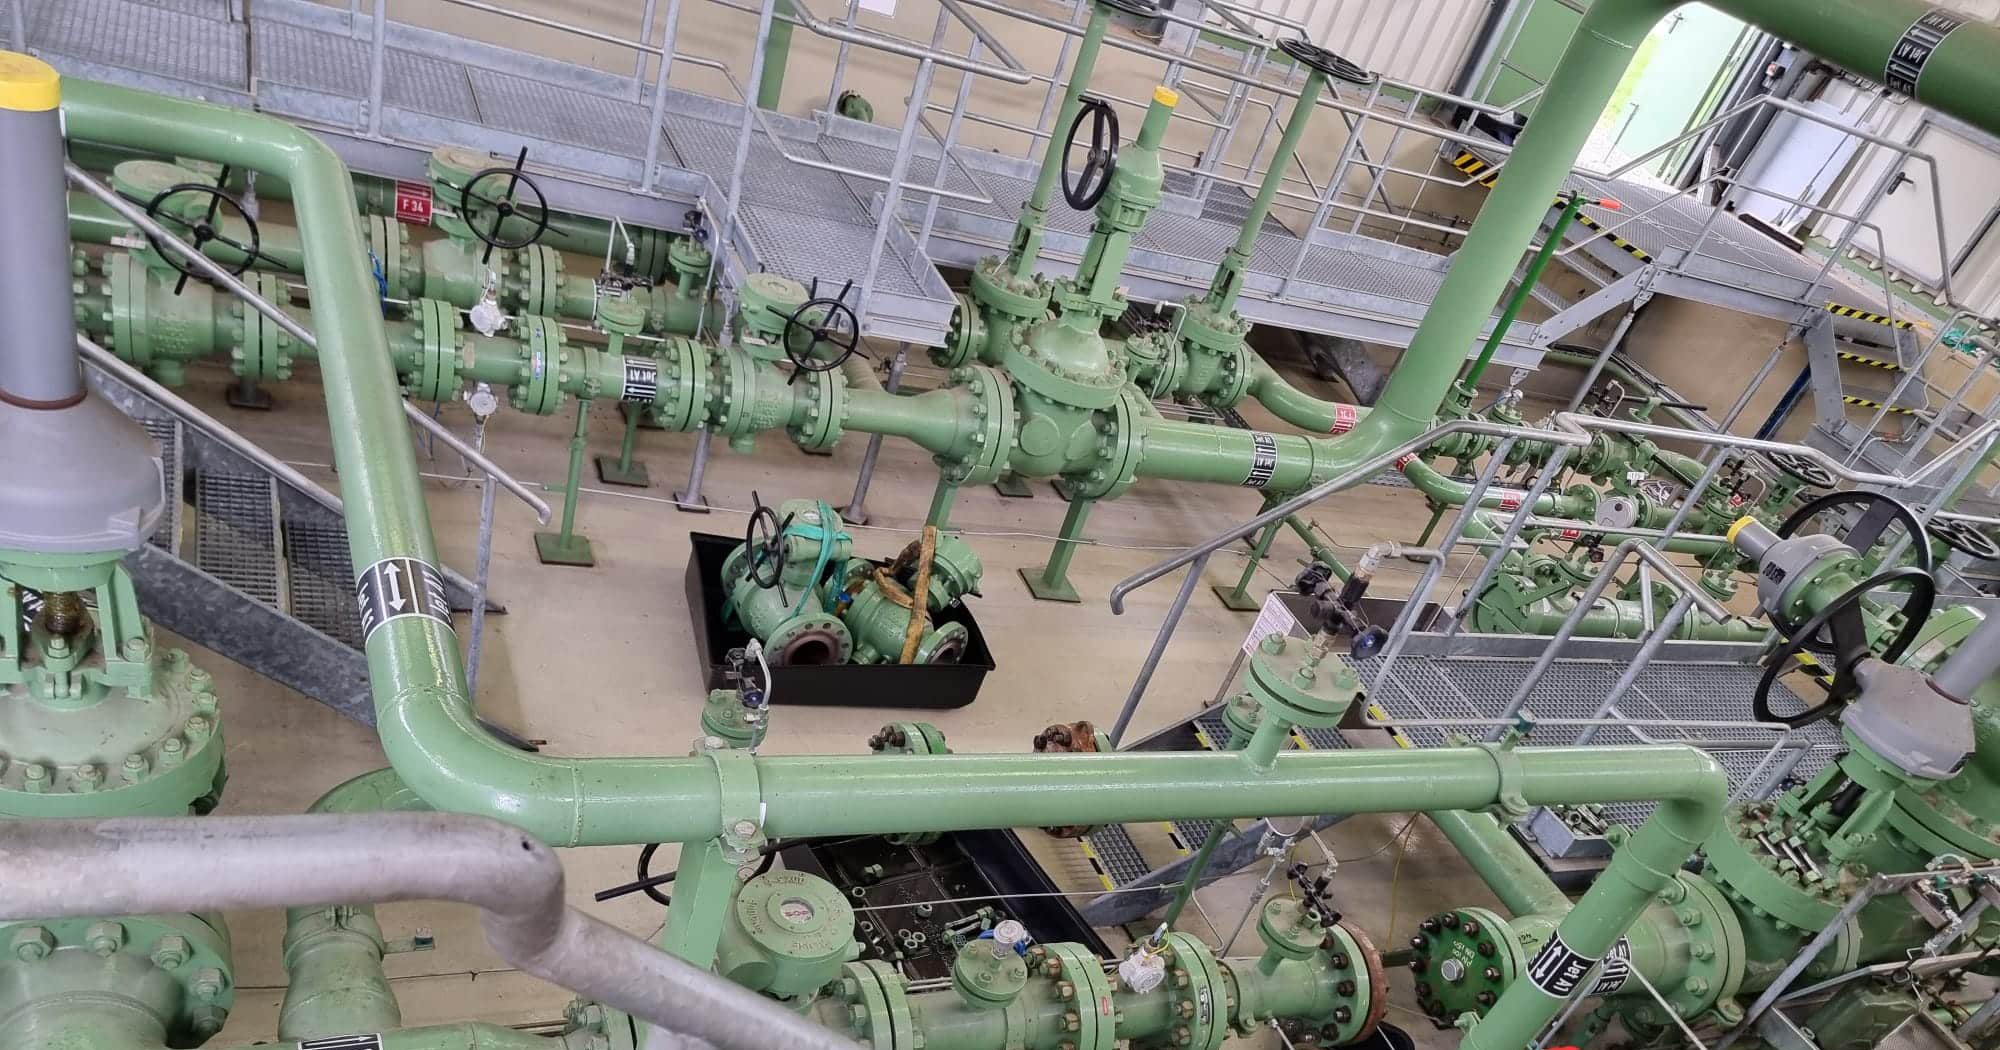
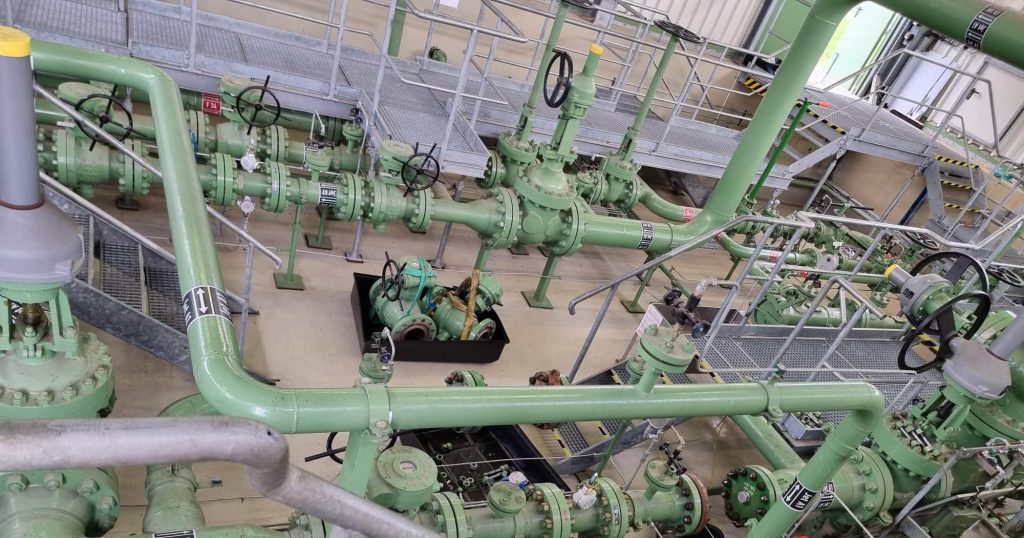
WFR engineered and deployed a compact separation spread at the receiving station, integrated with the client’s pig receiver, storage tank and silencer.
- Pig receiving and flow control. The spread tied into the 4 inch 600# pig receiver through a 4-1/16″ 10K ESD valve with a dedicated control panel, followed by a 3-1/16″ 10K choke manifold with a 2 inch choke for backpressure control on the incoming stream.
- Seperation. A 33m³ V2 vessel, rated to 7 barg, formed the core of the package. The vessel separated the kerosene from the nitrogen, with a control valve maintaining 2.8 barg on the gas outlet to regulate pig speed.
- Liquid handling. Recovered kerosene was routed to a 70 m³ client tank over a 30 meter transfer line, from where it was pumped back for reinjection into the pipeline.
- Nitrogen venting. The separated nitrogen was discharged to atmosphere through the client’s silencer, removing the need for a flare on a site close to the public.
- Safety systems. The package was protected by pressure safety valves set at 7 barg, a high pressure shutdown at 5.5 barg closing the ESD valve, and a high level alarm on the vessel at 80%. Wireless pressure and tem
- perature transmitters provided real time monitoring across the spread.
Execution
The request came in at short notice, with mobilization required within days of the enquiry. WFR compiled the equipment package, completed the engineering Intero, and mobilized the spread to the site in Belgium.
A crew of four WFR operators per shift ran the separation package throughout the operation. The choke and control valve settings were managed continuously to hold the pig at a stable speed over the pipeline route, while the vessel level and gas outlet pressure were monitored in real time through the data acquisition system.
The pipeline product transitioned from nitrogen to kerosene at the receiving station as the pig arrived, and the crew adjusted the separation parameters through each phase: nitrogen venting, mixed phase arrival, and full liquid flow.
The operation was completed safely.
The operation achieved all client objectives.
- Approximately 700 m³ of kerosene recovered and separated from nitrogen
- Stable pig speed maintained through controlled backpressure
- Nitrogen vented safely through the silencer, with no flaring required
- Continuous real time monitoring of pressures, temperatures and vessel level
All operations performed safely
This project demonstrates WFR’s capability to deliver engineered separation solutions for pipeline operations, beyond conventional well testing. The package was designed, mobilized and executed at short notice, in close cooperation with the client and the engineering partner.
The operation serves as a reference project for pipeline refill and recommissioning support, and marks the start of WFR’s working relationship with Intero Integrity Services.